Custom racks and enclosures in sheet metal, built to your drawing.
Send us the drawing. We laser cut, form, weld, coat and assemble custom racks, containment and enclosures for data center OEMs. Banja Luka to Germany, Austria and Italy by truck in 1–2 days.
- 350 people
- 20,000 m² in two plants
- 30+ technologies in-house
- 3,000 m² assembly area
- Since 1994
- Series in 4–8 weeks
- Bending up to 4 m
- EUR.1 — no EU duty
Problems we solve for data center OEMs
We do not design your product. We make sure it can be built, in volume, close to you.
Capacity does not keep up with the AI build-out.
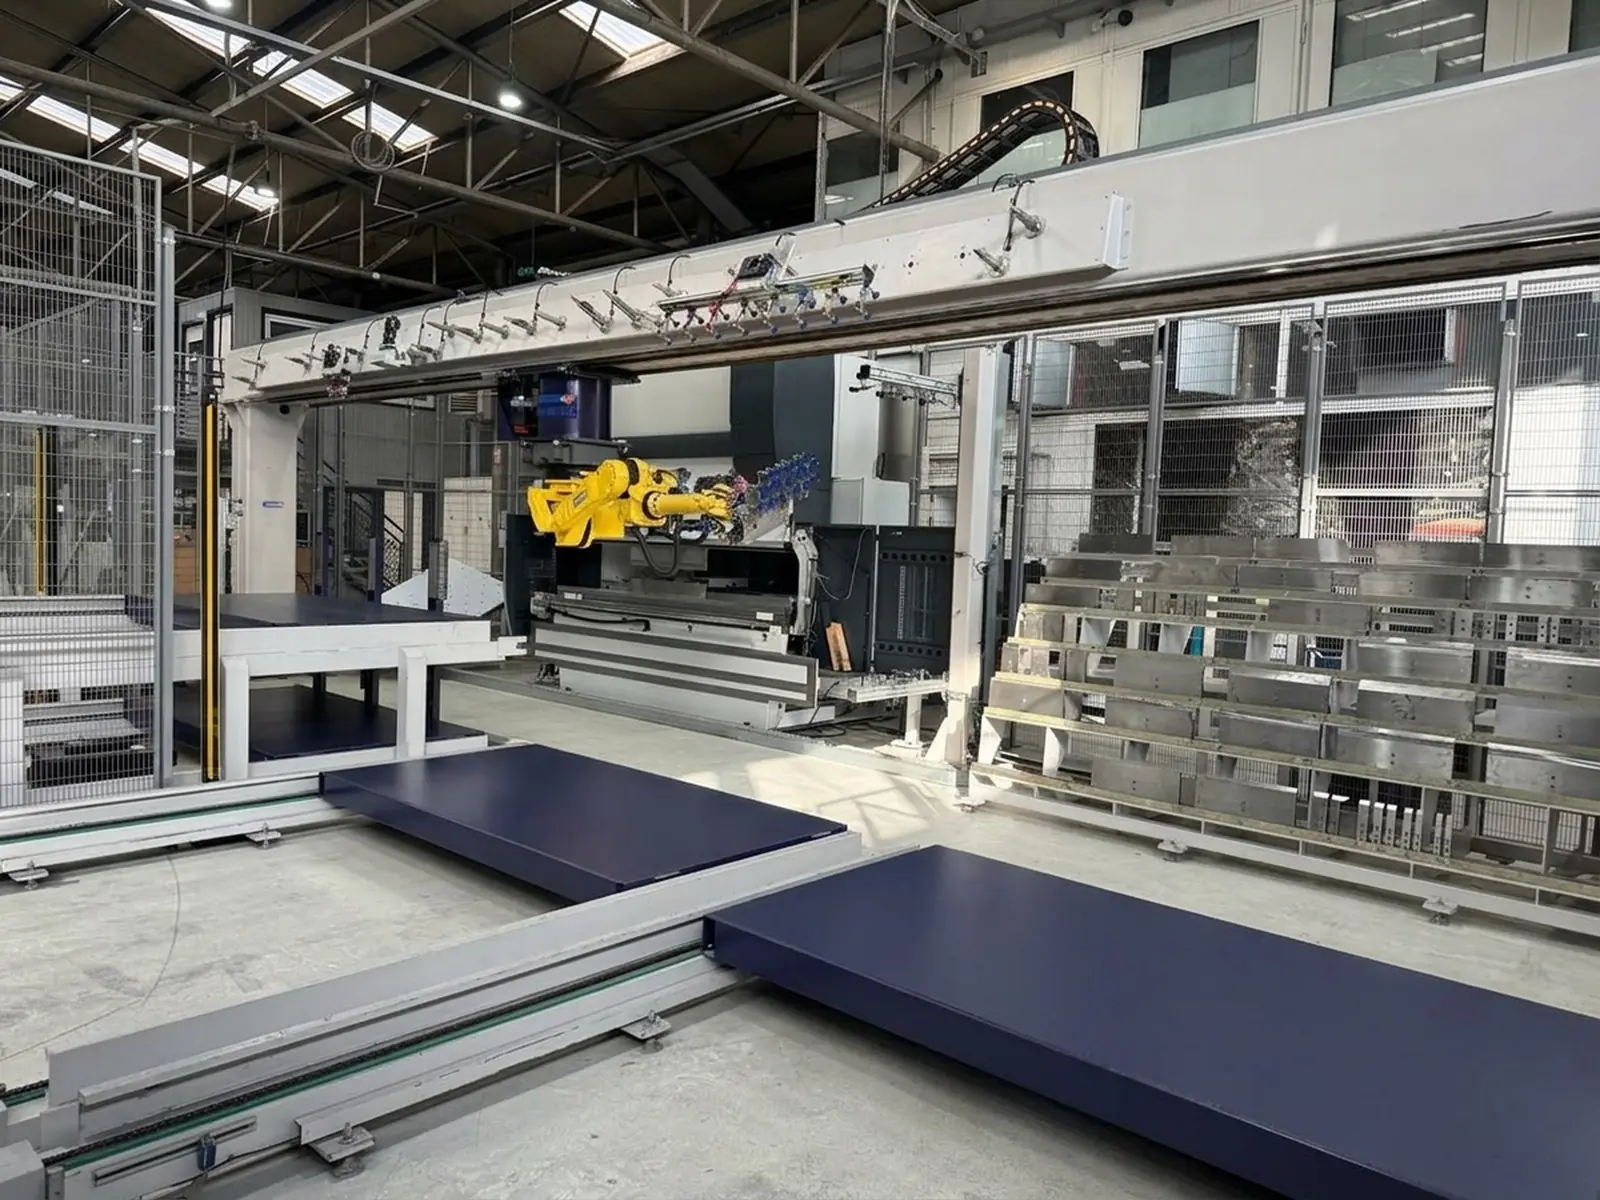
A 350-person plant with three LVD fiber lasers (4, 6 and 12 kW), a combined laser-punch machine and a punch press, fed by an automated sheet store and run as a series operation.
Capacity equal to 1,000 racks a month
Long lead times and risk from overseas supply.
Production in Europe, no ocean freight: short series lead times of 4–8 weeks, then 1–2 days by truck to Germany, Austria and Italy.
Series lead time 4–8 weeks
Too many suppliers for one assembly.
Cutting, forming, welding, hardware, powder coating, assembly and wiring under one roof and one purchase order.
30+ technologies in one plant
Long panels and heavy frames that other shops avoid.
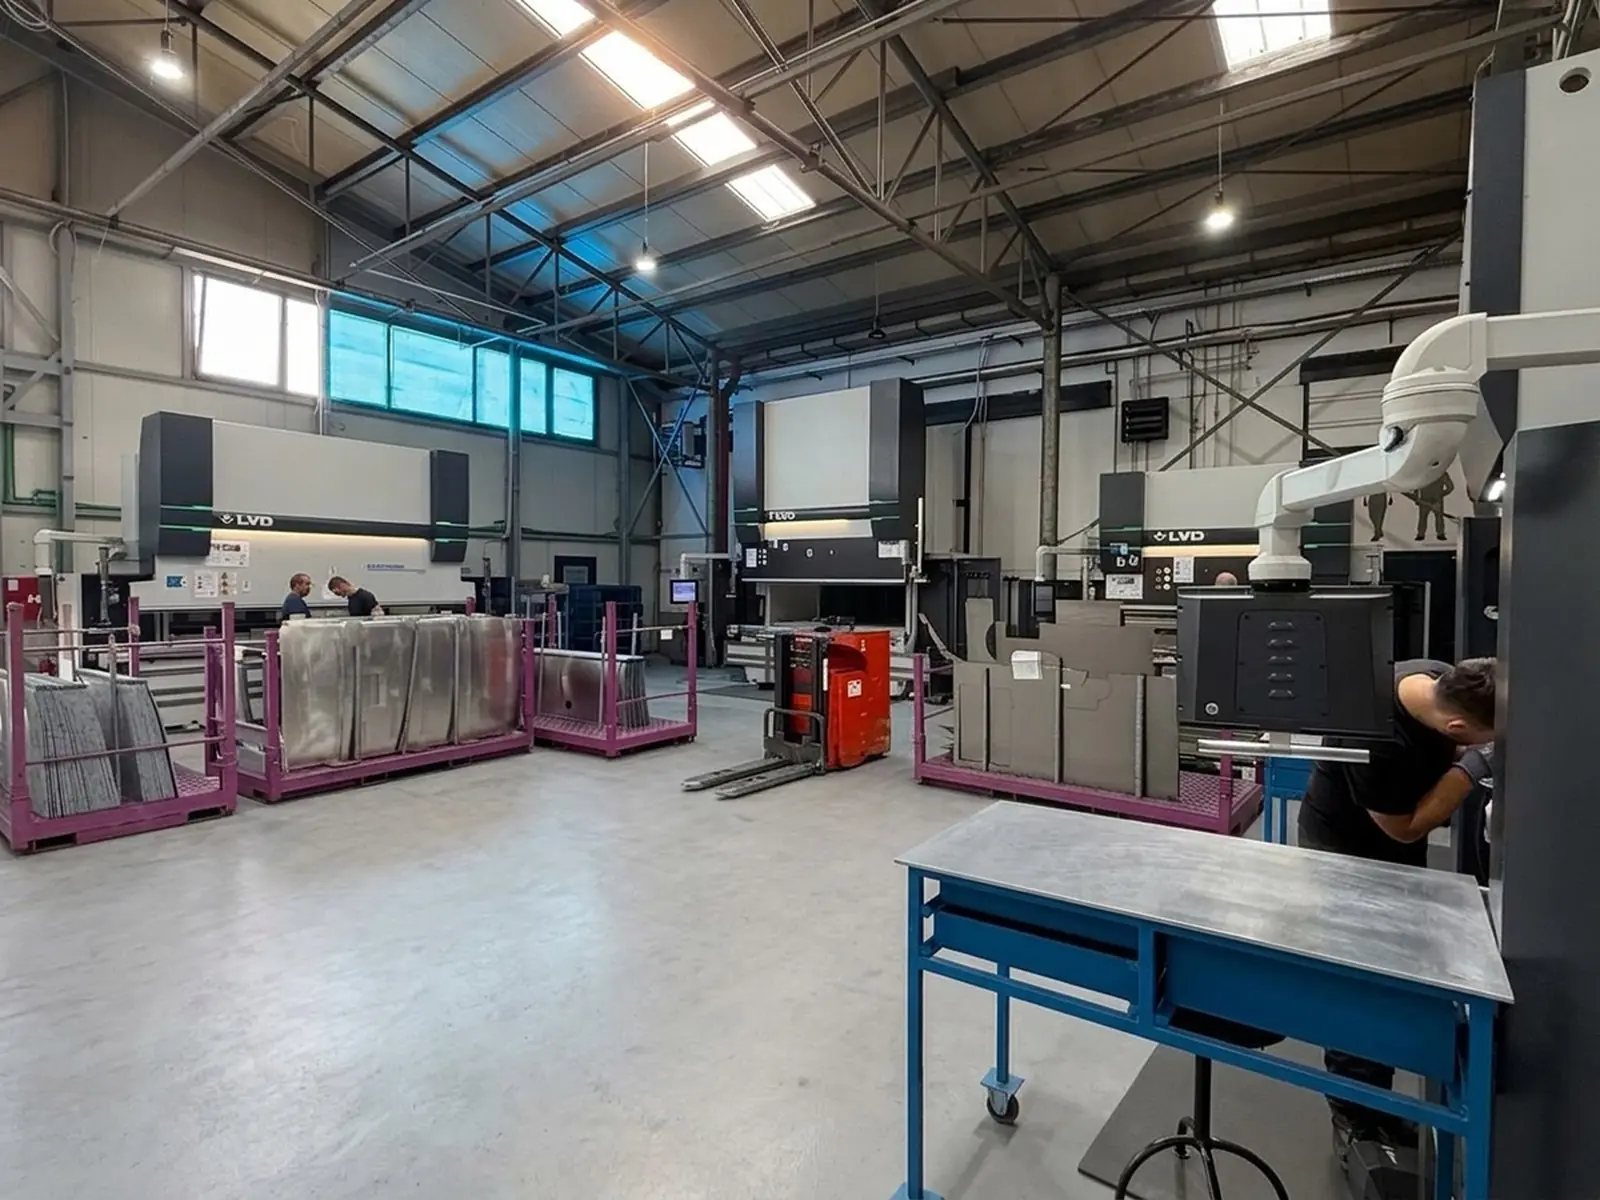
13 press brakes with bending lengths up to 4 m — long cable trays and profiles in one piece — plus 2 robotic bending cells, robotic and laser welding, and a powder line for parts up to 6 m.
Bending up to 4 m
Quality you have to be able to audit.
Certified welding, incoming, in-process and final inspection, traceability from raw material to delivery, 8D for nonconformities.
ISO 9001:2015 · EN ISO 3834-2 · EN 15085-2 CL1 · EN 1090-1 · DIN 6701
Changes, prototypes and new variants.
An in-house development team takes a part from concept or first drawing to a stable series process.
Prototype to series in the same plant
The line your part runs through
More than 30 technologies under one roof. The eight core stations below show how a part moves from sheet to assembled unit without leaving the plant, so tolerances, finish and lead time stay in one hand.
Six technologies, one part
Select a station to see the mark it leaves on the part: contour, perforation, bends, fasteners, welds and finish.
- ST‑01
Automated sheet store
Your material is stocked, identified and fed to the machines without manual handling.
LVD WAS · feeds lasers and punching
- ST‑02
Fiber laser cutting
Outer contour, cut-outs, slots and tabs — straight from your DXF.
3 LVD fiber lasers · 4, 6 and 12 kW
- ST‑03
Punching
Perforation for airflow, louvres, knock-outs and formed features.
Laser-punch combi + punch press · up to 6.35 mm
- ST‑04
Bending
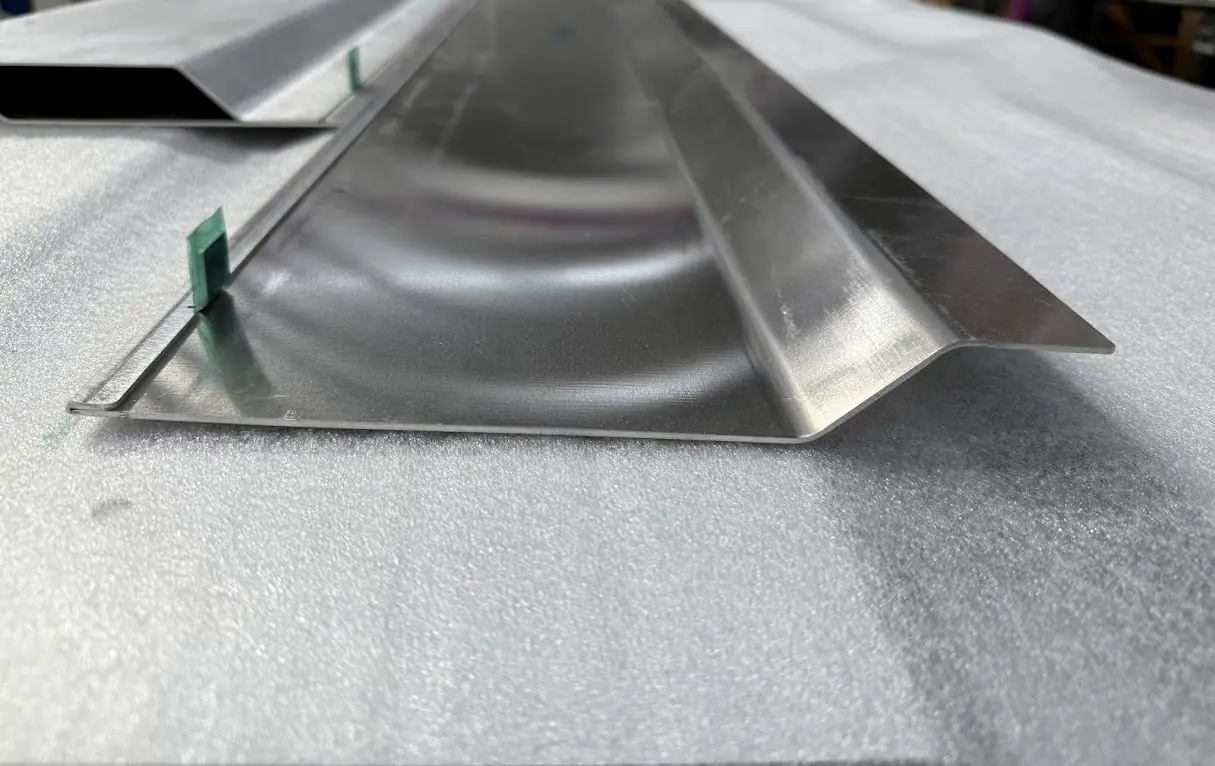
Flanges, long profiles and cable trays, full-length panels, robotic and automated panel bending.
13 presses · 0.8–4 m · 2 robotic cells · XLTbend
- ST‑05
Hardware insertion
Self-clinching nuts, studs and standoffs, stud welding.
PEM-type fasteners · stud welding
- ST‑06
Welding
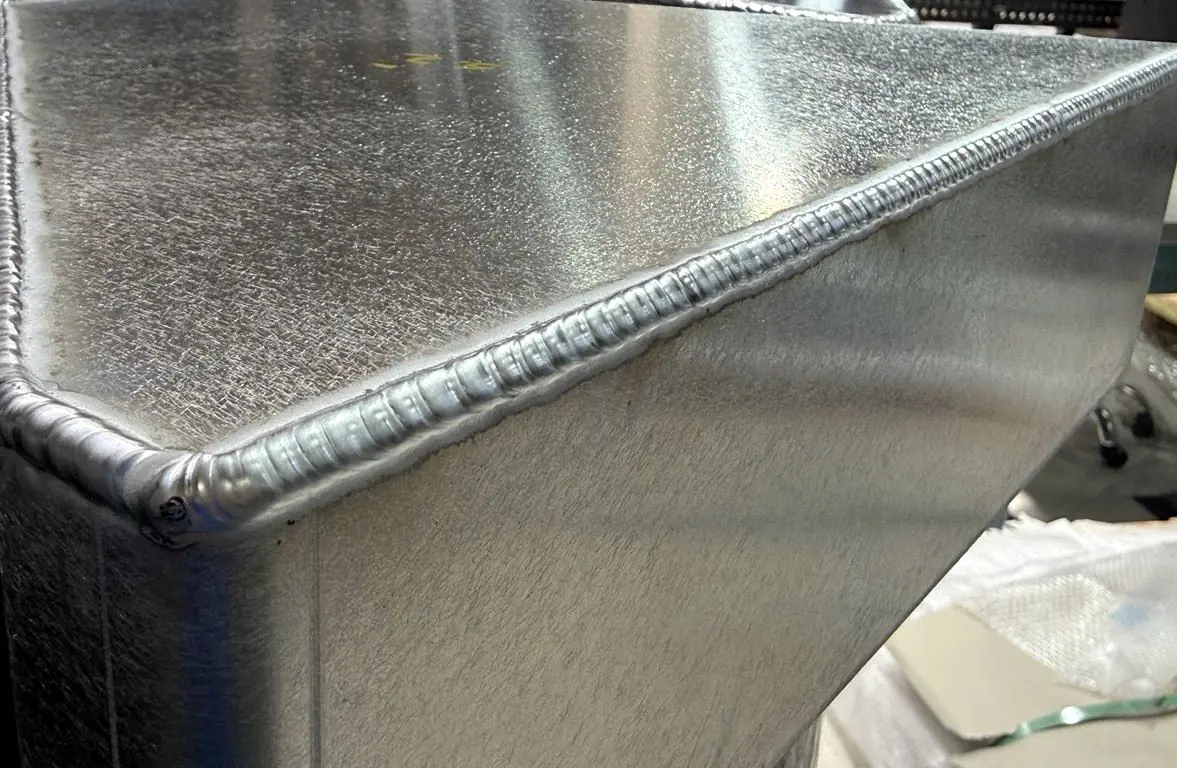
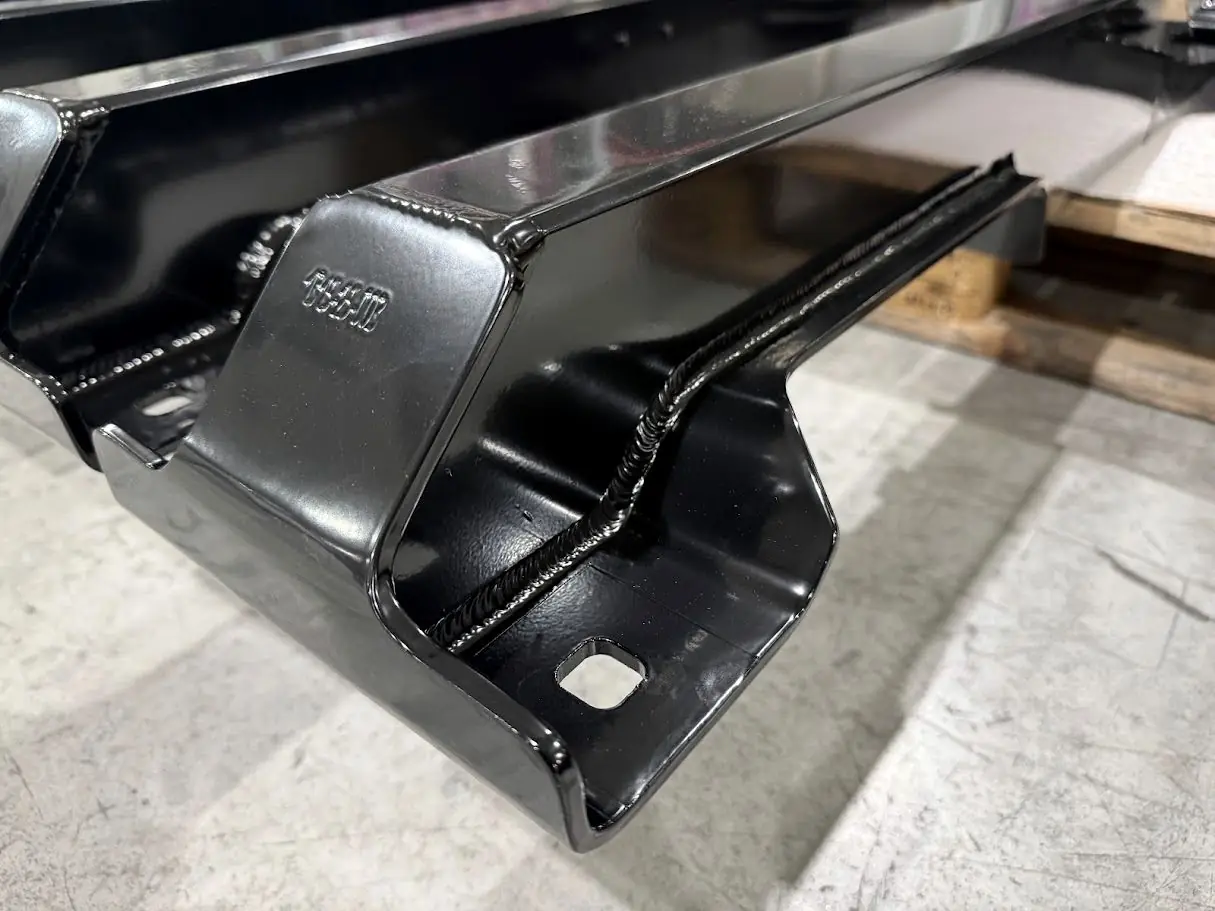
Closed corners, frames and structures — robotic or manual, steel, stainless, aluminium.
Robotic · MIG/MAG · TIG · laser · spot
- ST‑07
Powder coating
Durable finish in the colour you specify, e.g. RAL 9005 or 7035.
Automated line · parts up to 6 m
- ST‑08
Assembly & wiring
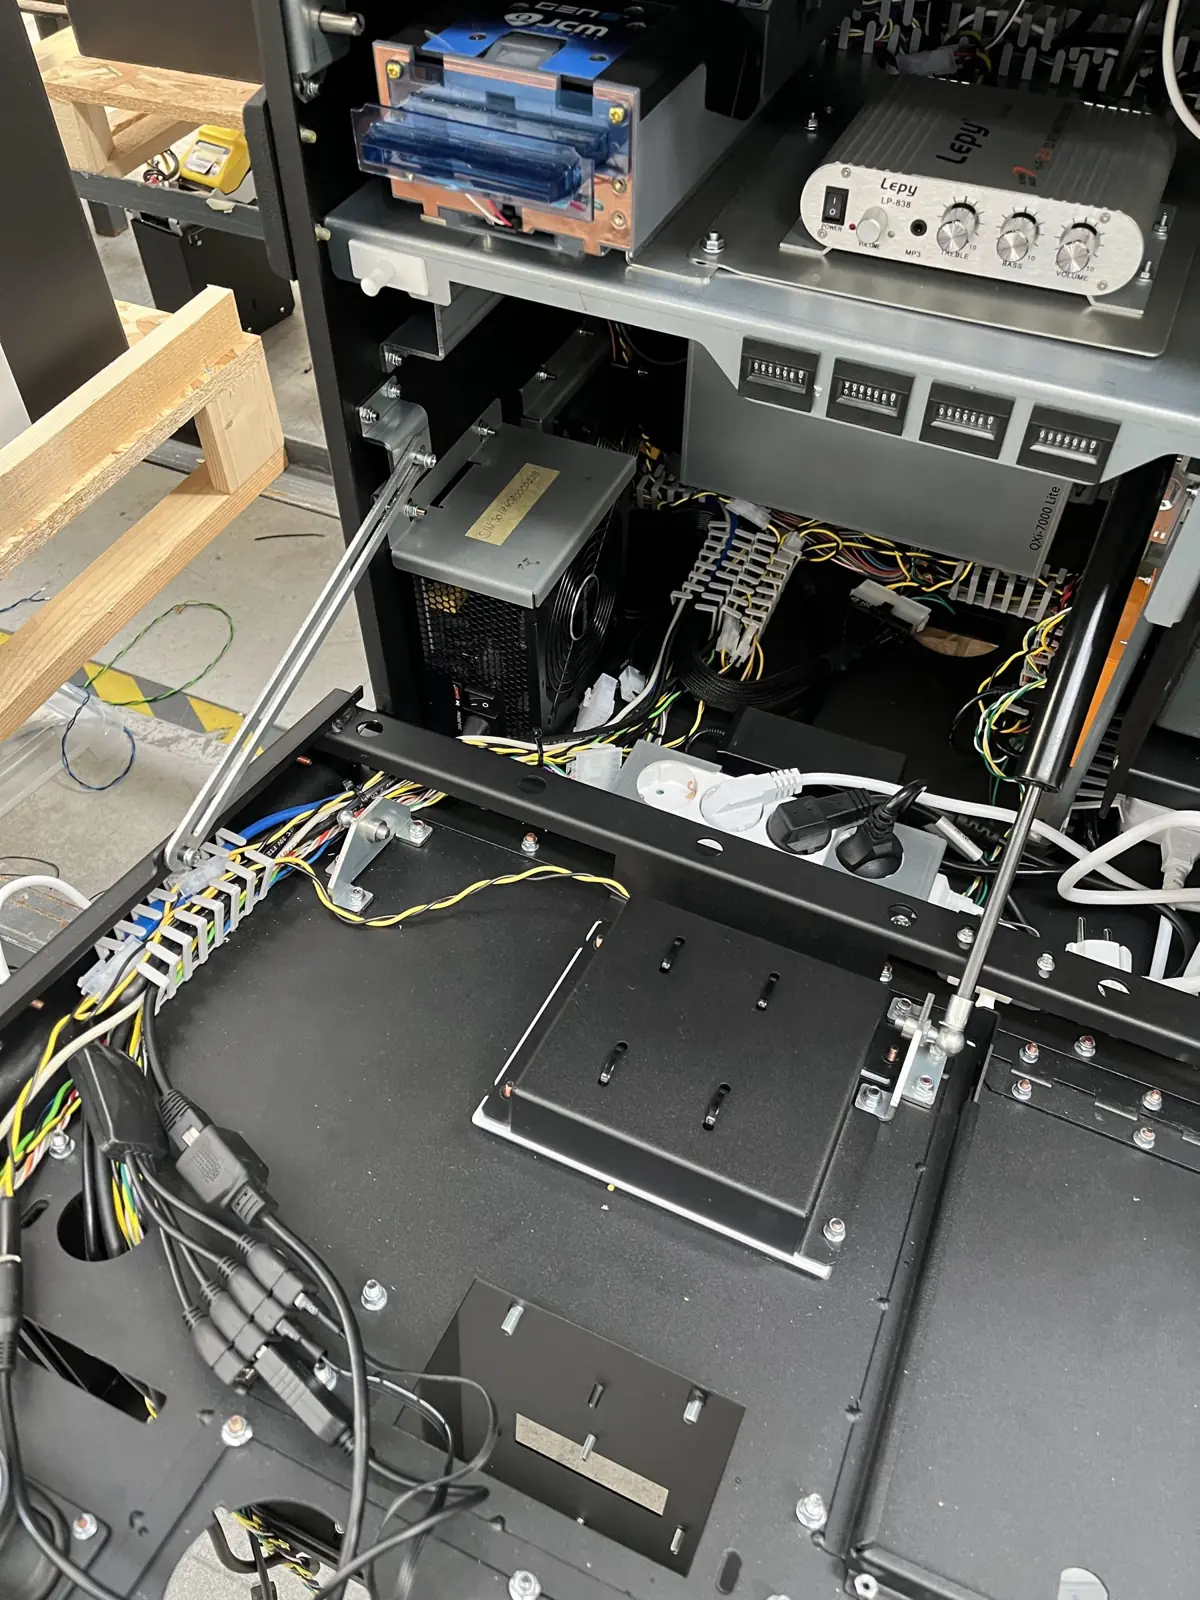
Sub-assemblies, cabling and electrical test, packed for your line.
Final assembly · cabling · test
Where our parts end up
Typical data center hardware built from sheet metal. We build to the customer's drawing; if your part is not listed, it can still be a fit.
Sheet-metal cable managers and overhead power distribution in a data center (stock photos)
| Application | Examples | Laser | Punch | Bend | Weld | HW | Coat | Assy | Processes |
|---|---|---|---|---|---|---|---|---|---|
| Server & network rack components | Rack frames, doors, 19" rails, server and GPU chassis | Laser · Punch · Bend · Weld · Hardware · Coat · Assembly | |||||||
| Aisle containment parts | Door frames, roof frames, fillers, partitions | Laser · Punch · Bend · Weld · Coat | |||||||
| Enclosures for power equipment | UPS and battery cabinets, tap-off boxes, RPP | Laser · Punch · Bend · Weld · Hardware · Coat · Assembly | |||||||
| Chassis for cooling equipment | CDU and in-row chassis, manifold brackets | Laser · Punch · Bend · Weld · Coat | |||||||
| Edge & modular data centers | Outdoor cabinets, micro DC, skid frames | Laser · Punch · Bend · Weld · Hardware · Coat · Assembly |
Quality and delivery you can check
Typical terms for a new part, confirmed in every quotation. Series lead time 4–8 weeks.
Incoming inspection
Materials and certificates verified before production.
In-process control
First-article checks at laser, punch and press brake.
Final inspection
Visual and dimensional check before packing, inspection report with the sample.
Traceability & 8D
Raw material to delivery; structured corrective actions.
- Day 0Drawing or requirement received
- ≈ Day 7Quotation with DFM notes
- ≈ Day 30Sample with inspection report
- SeriesFrom 500 pcs · 4–8 weeks
Reference: railway industry
ELAS supplies Stadler with interior components for rail vehicles — ceiling systems, air ducts and aluminium welded assemblies built to EN 15085-2 CL1, the highest certification level for welding rail vehicles. Data center parts run through the same plant and the same quality system.
- Customer
- Stadler (rail vehicles)
- Parts
- Ceiling systems, air ducts, aluminium welded assemblies
- Standard
- EN 15085-2 CL1 · EN 17460 / DIN 6701 bonding
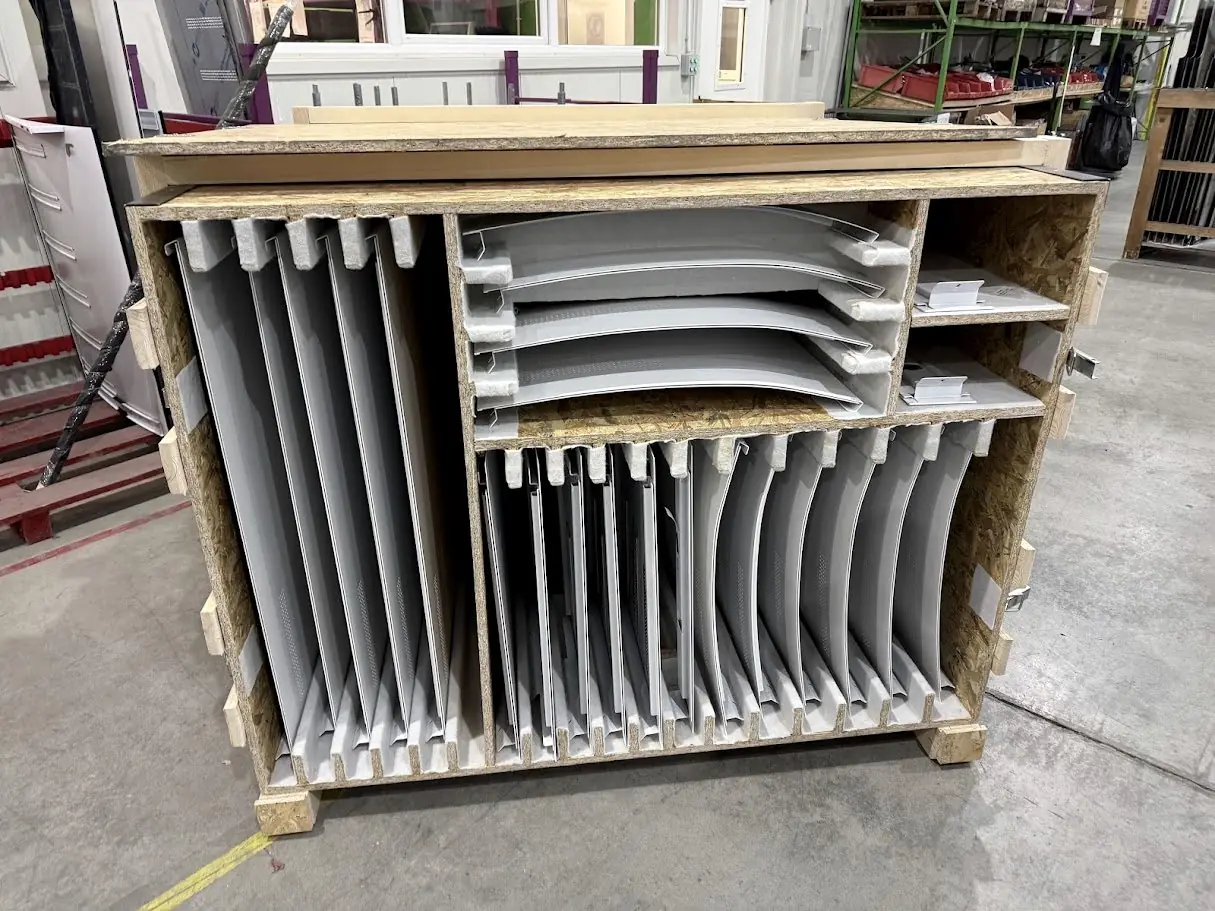
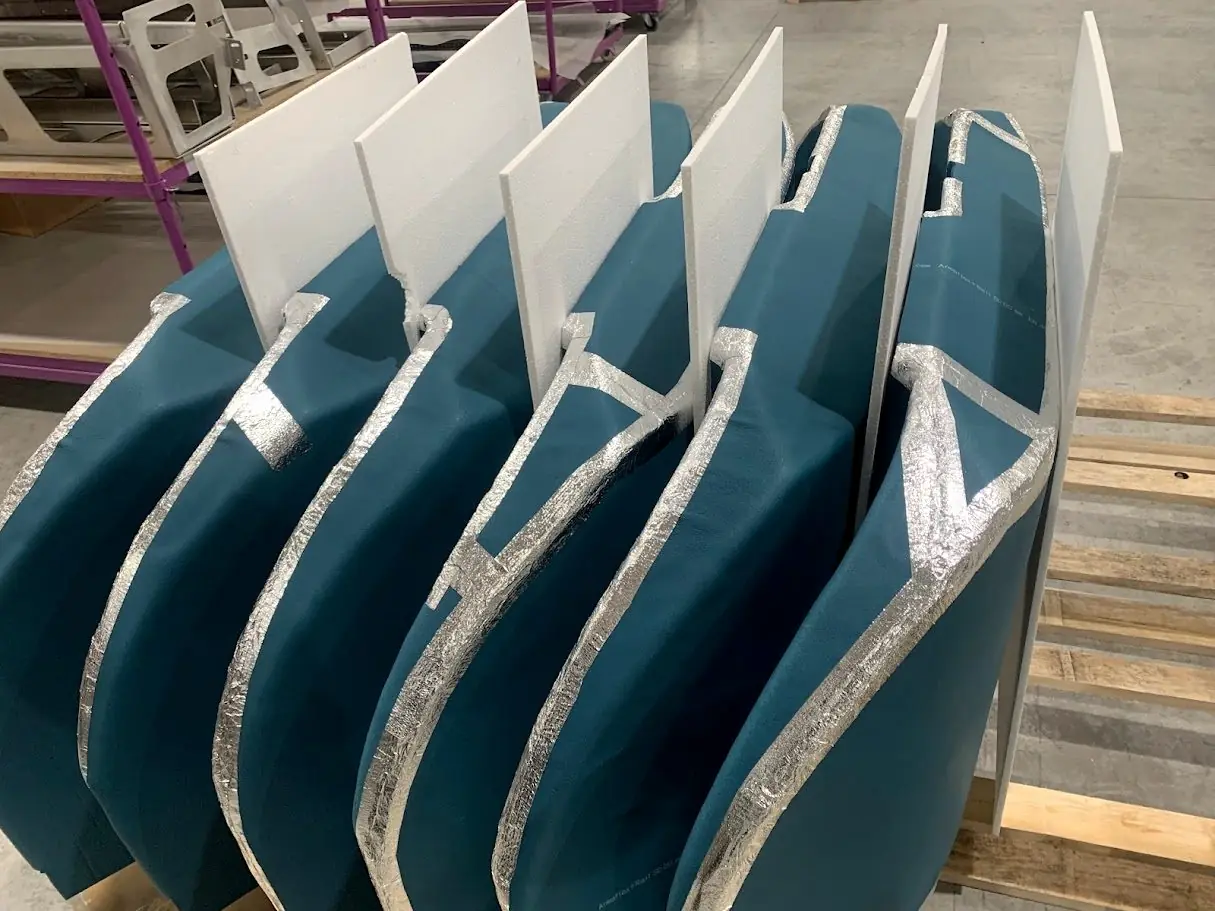
The plant
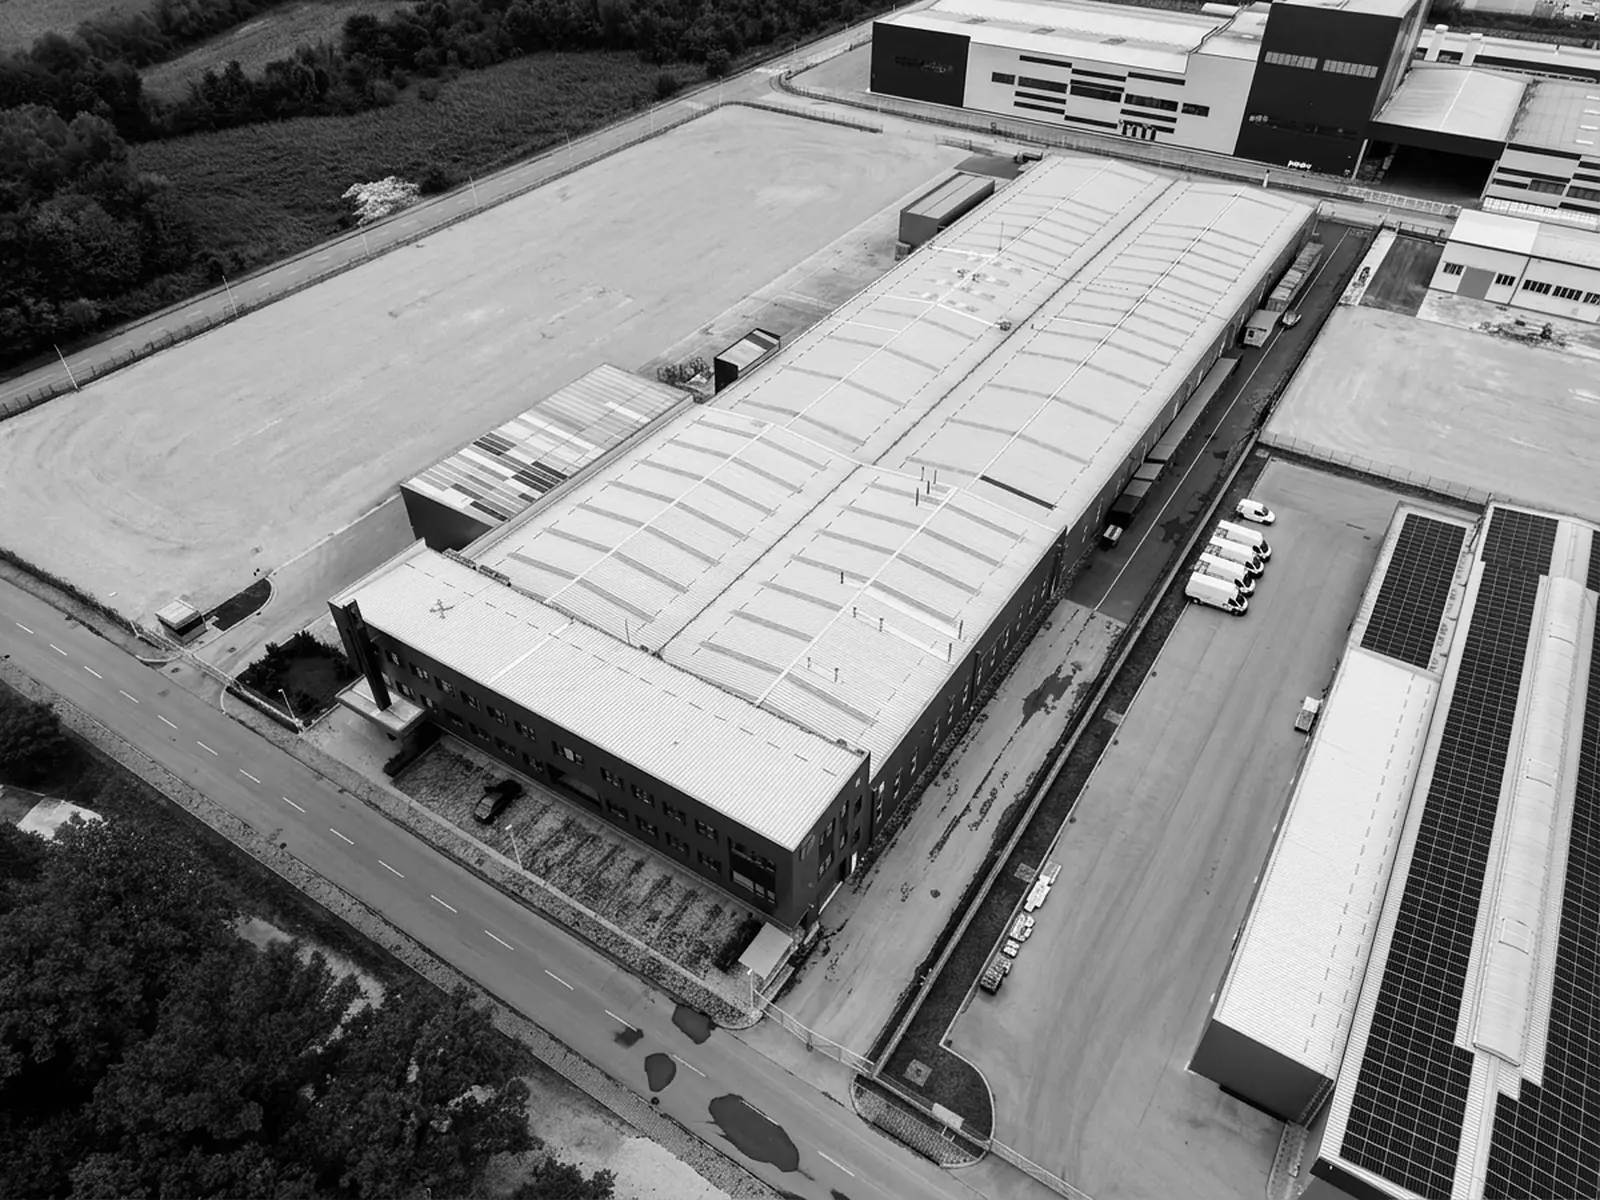
Two sites in Banja Luka with 20,000 m² of production and assembly halls. More than 30 manufacturing technologies in-house, new LVD lines since 2025. Exports since 1994 to Germany, Austria, Switzerland, Denmark, the UK and the USA.
- Sheet storage
- Automated LVD WAS store feeding the lasers and punching
- Fiber lasers
- 3 × LVD · 4, 6 and 12 kW · sheets up to 3,050 × 1,525 mm
- Punching
- LVD laser-punch combination machine + punch press · up to 6.35 mm · perforation and louvres
- Press brakes
- 13 presses · bending length 0.8–4 m · 2 robotic bending cells · automated XLTbend panel bending
- Welding
- Robotic cells · MIG/MAG · TIG · laser · spot · steel, stainless, aluminium
- Hardware
- Self-clinching nuts, studs and standoffs · stud welding
- Powder coating
- Automated electrostatic line · parts up to 6,000 mm · wet paint booth
- Assembly
- Final assembly, cabling and electrical test
Customs: every EU shipment travels with an EUR.1 movement certificate, so EU customers pay no import duty — the same as for goods made in the EU. USA: shipped by sea container; our goods currently carry a 10% US import tariff.
Full plant datasheet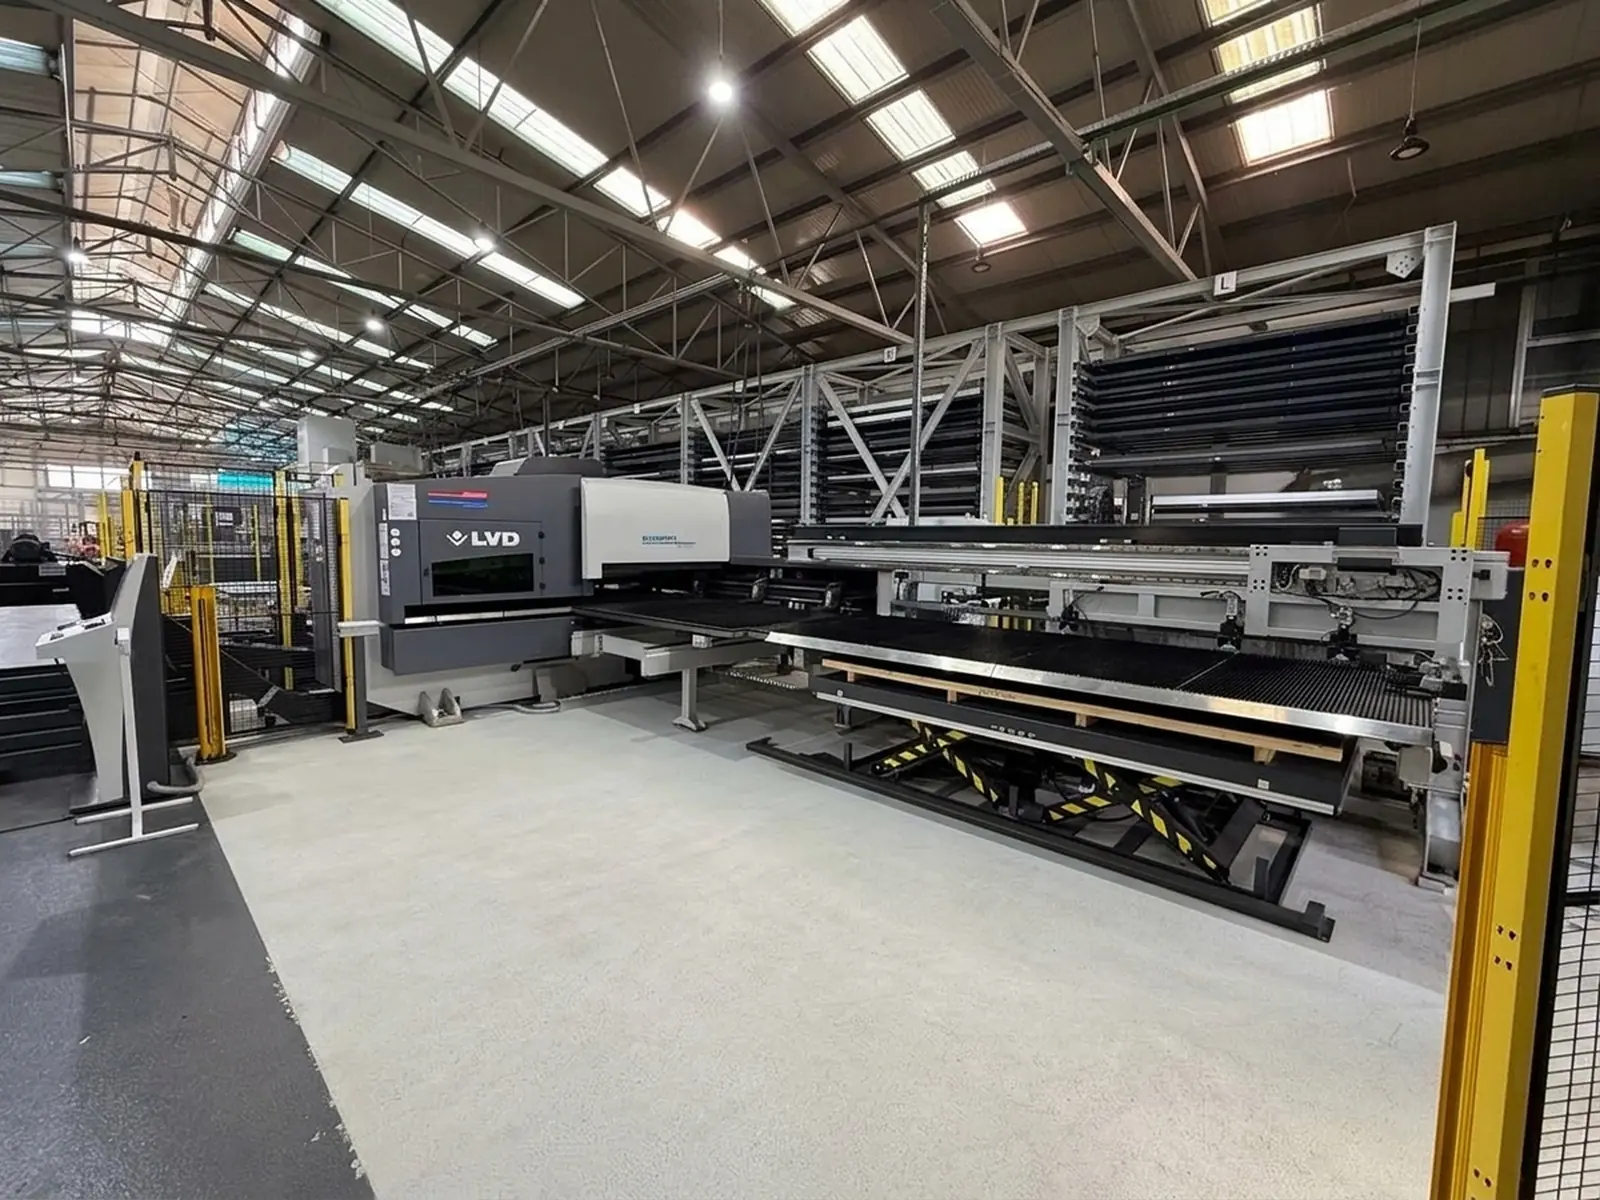
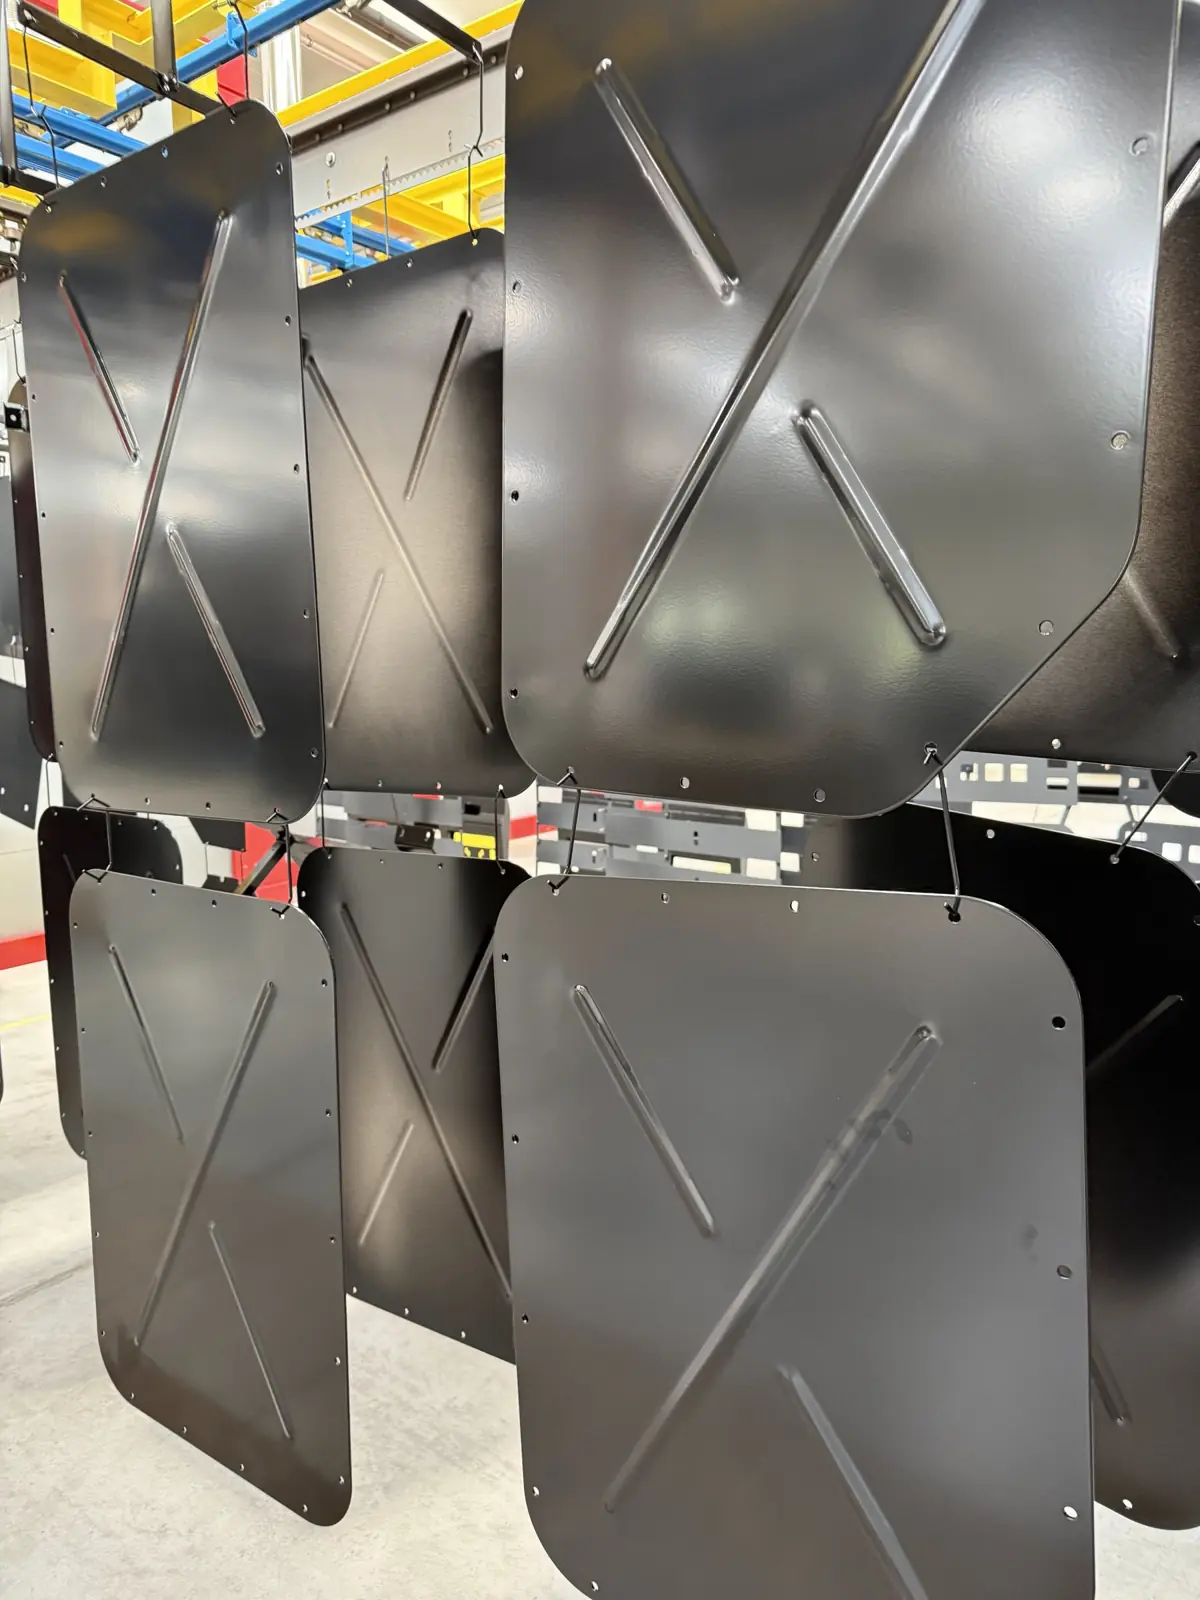
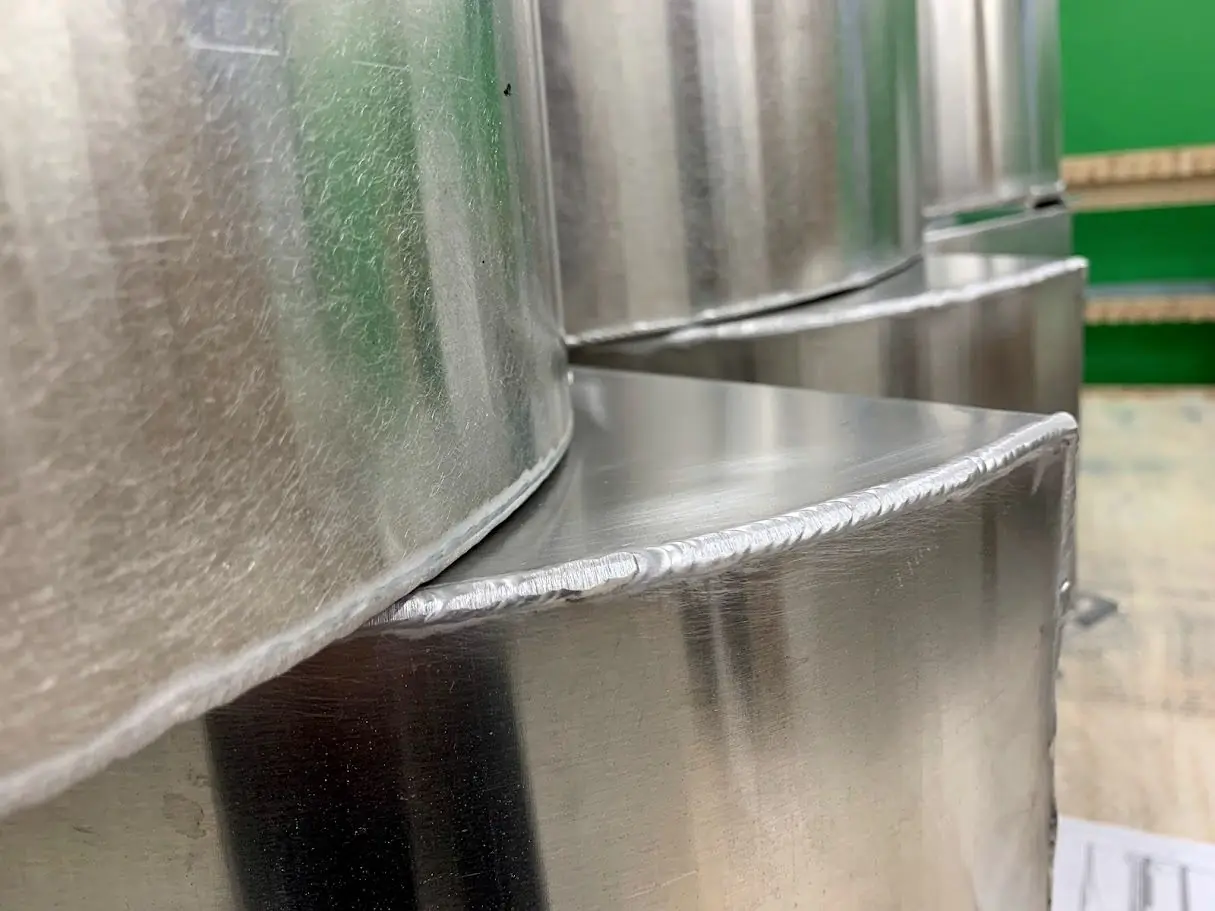
From our floor
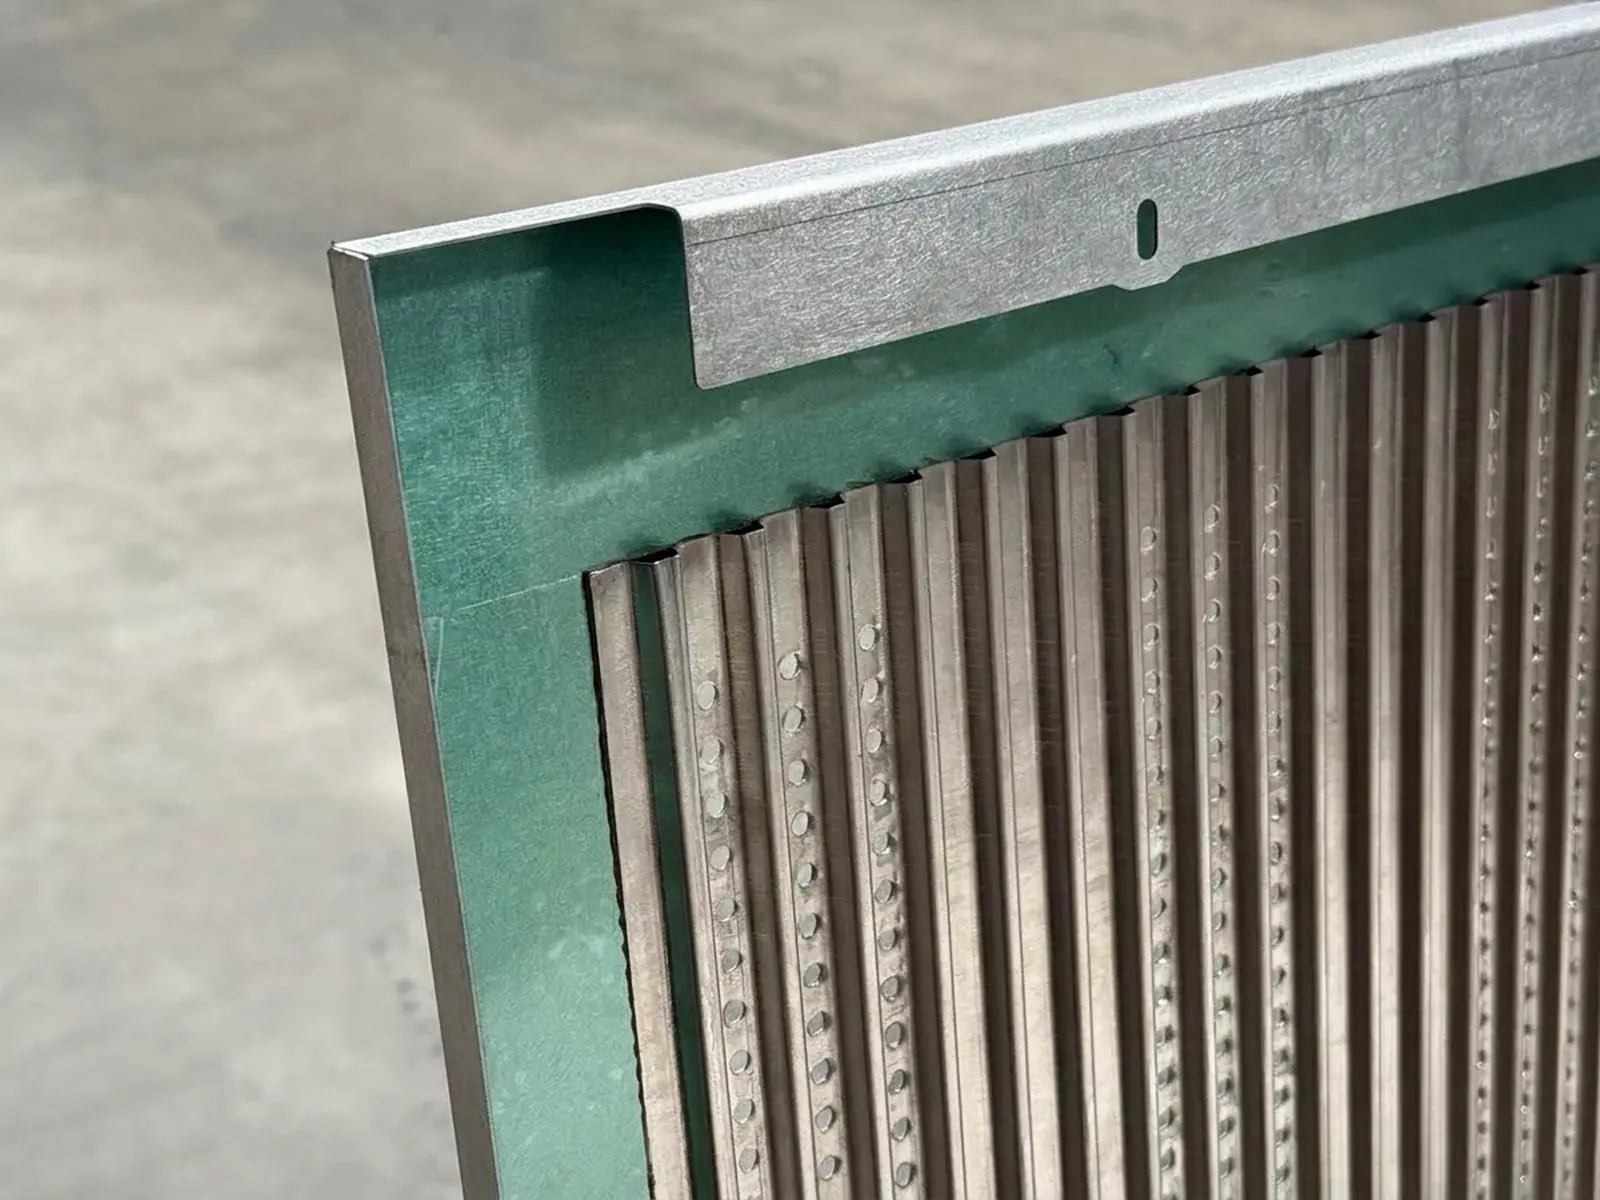
Talk to our engineering team.
Tell us what you are working on — a drawing, a capacity question or a part that is hard to source today. An engineer will get back to you.
Talk to our engineers- Your input
- Drawing, model or requirement
- Manufactured by
- ELAS d.o.o., Banja Luka
- Certified
- ISO 9001:2015EN ISO 3834-2EN 15085-2 CL1EN 1090-1DIN 6701
- Delivery
- Truck to DE · AT · IT
- Contact
- sales@elas.ba